Die casting mold work under high temperature, high pressure, and repeated thermal cycles.
Therefore, even a well-designed mold can develop problems after long-term production.
Common die casting mold problems include flash, mold sticking, erosion, cracks, poor venting, cooling problems, core damage, and dimensional deviation.
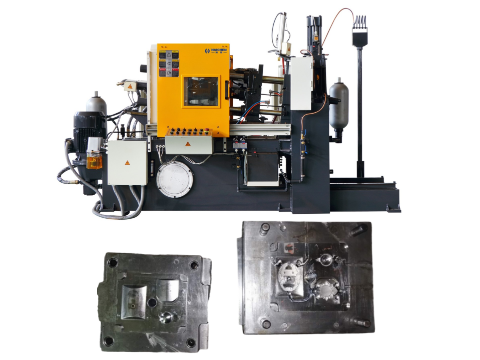
These problems can affect casting quality, cycle time, mold life, and production costs.
Fortunately, most problems can be reduced through proper mold design, temperature control, process adjustment, and regular maintenance.
This guide explains the most common die casting mold problems, their causes, and practical solutions.
What Is a Die Casting Mold?
A die casting mold, also called a die, is a precision tool used to form molten metal into the required shape.
A typical die includes:
- Fixed die half
- Moving die half
- Mold cavity
- Core
- Runner system
- Gate
- Overflow
- Venting system
- Cooling channels
- Ejector system
During production, molten metal enters the cavity at high speed and pressure.
Meanwhile, the mold controls the metal flow and removes heat from the casting.
As a result, mold design has a direct influence on casting quality and production efficiency.

Poor Mold Venting and Porosity
Poor venting is one of the most common problems in high-pressure die casting.
During filling, the molten metal pushes air and gases through the cavity.
If the venting system cannot remove these gases effectively, air can become trapped inside the casting.
As a result, the casting may develop:
- Gas porosity
- Blowholes
- Internal voids
- Surface bubbles
- Reduced mechanical strength
Causes
Common causes include:
- Insufficient venting area
- Incorrect vent location
- Blocked vents
- Excessive release agent
- High filling speed
- Poor vacuum performance
Solutions
First, check whether the vents are clean and large enough.
Next, review the filling simulation and determine where air is likely to become trapped.
In addition, manufacturers can use overflow wells and vacuum-assisted die casting when the application requires better internal quality.
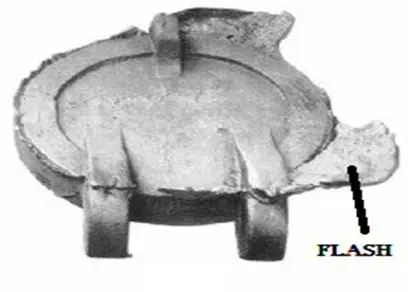
Die casting mold Flash and Burrs
Flash occurs when molten metal enters the gap between mold surfaces.
It usually appears around:
- Parting lines
- Slides
- Inserts
- Ejector pins
- Core areas
Excessive flash increases trimming work and may also affect dimensional accuracy.
Main Causes
The most common causes are:
- Insufficient clamping force
- Excessive injection pressure
- Damaged parting surfaces
- Mold misalignment
- Mold wear
- Incorrect mold installation
How to Fix Mold Flash
First, inspect the parting surface for wear or damage.
Then, check the mold alignment and machine clamping force.
If the mold has been used for a long time, the parting surface or core may require repair.
Importantly, simply increasing machine clamping force is not always the correct solution. The actual cause should be identified first.
Die Sticking
Die sticking occurs when the casting remains attached to the mold instead of being released normally.
This problem can slow down production and may damage both the casting and the mold.
Why Does Die Sticking Happen?
Common reasons include:
- Poor draft angle
- Excessive mold temperature
- Incorrect release agent
- Rough cavity surface
- Alloy adhesion
- Mold damage
For example, zinc alloys can adhere to damaged or improperly treated mold surfaces.
Solutions
Check the draft angle and cavity surface condition first.
Then, inspect the spraying system and make sure the release agent is applied evenly.
If sticking continues, review the mold temperature and alloy filling conditions.
Surface treatment such as nitriding or other suitable coatings may also improve mold wear resistance in some applications.
Die casting Mold Erosion and Wear
Die casting molds are exposed to repeated high-speed metal flow.
Therefore, areas around the gate, runner, and cavity can gradually wear or erode.
Mold erosion may lead to:
- Dimensional changes
- Surface defects
- Flash
- Shorter mold life
- Unstable production
Main Causes
The main causes include:
- High metal velocity
- High metal temperature
- Repeated thermal cycling
- Poor mold steel selection
- Improper heat treatment
Solutions
Inspect high-wear areas regularly.
At the same time, optimize the gate design and metal flow speed.
For high-volume production, selecting suitable hot-work die steel and heat treatment is also important.
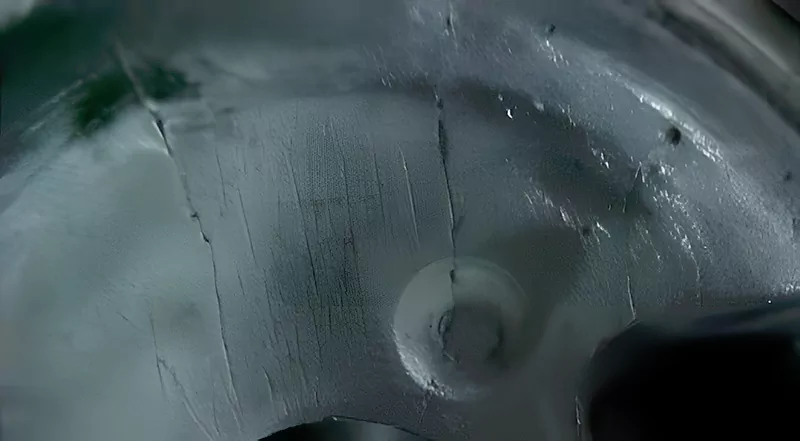
Die casting Mold Cracks and Heat Checking
Repeated heating and cooling create thermal stress in the die.
Over time, this stress can produce small cracks on the mold surface, often called heat checking.
These cracks may become deeper and eventually damage the mold.
Common Causes
- Excessive thermal cycling
- Large temperature differences
- Poor cooling design
- Incorrect preheating
- Inappropriate mold steel
- Excessive local heat
How to Prevent Mold Cracks
Maintain a stable mold temperature during production.
Furthermore, avoid sudden temperature changes whenever possible.
The cooling system should also remove heat evenly rather than creating large temperature differences between different areas of the mold.
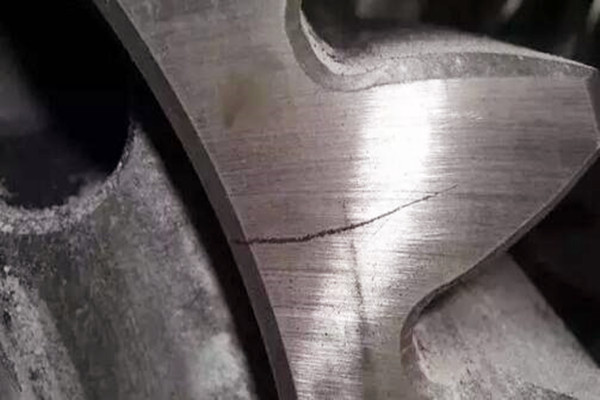
Die casting mold Cooling Problems and Warpage
The cooling system plays an important role in die casting mold performance.
If different areas of the mold cool at different rates, the casting may shrink unevenly.
As a result, manufacturers may see:
- Warpage
- Dimensional deviation
- Cracks
- Uneven surface quality
- Longer cycle times
Solutions
The cooling channels should match the casting geometry and thermal load.
In addition, monitor the inlet and outlet temperatures of the cooling system.
If one area remains too hot, local cooling may be required.
A mold temperature controller can also help maintain a more stable process window.
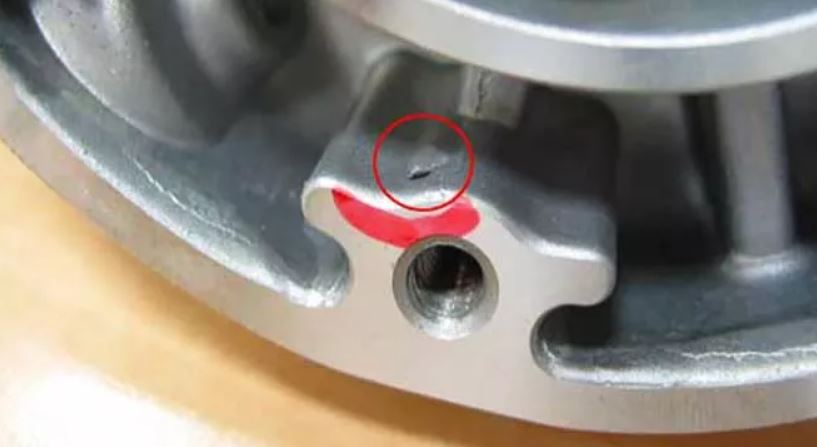
Cold Shut and Incomplete Filling
A cold shut occurs when two metal flow fronts meet but do not fuse properly.
Incomplete filling happens when molten metal fails to reach the entire cavity.
Both problems can reduce casting quality.
Common Causes
- Low metal temperature
- Low mold temperature
- Incorrect gate design
- Insufficient filling speed
- Poor runner design
- Excessive heat loss
Solutions
First, check the metal and mold temperatures.
Then, review the gate and runner design.
Increasing filling speed may help in some cases. However, excessive speed can also increase turbulence and air entrapment.
Therefore, the correct process window should be determined through testing or filling simulation.
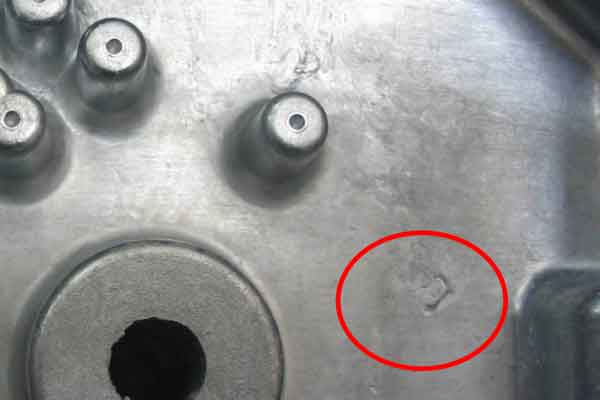
Dimensional Deviation
A die casting mold must maintain accurate alignment throughout production.
However, wear, thermal expansion, or incorrect installation can cause dimensional changes.
Typical Causes
- Mold misalignment
- Core wear
- Parting surface damage
- Uneven cooling
- Incorrect process parameters
- Thermal expansion
Solutions
Regularly inspect:
- Guide pins
- Guide bushes
- Core inserts
- Parting surfaces
- Ejector system
- Cooling channels
If the mold has significant wear, repair or replacement of the affected components may be necessary.
Ejector Pin Problems
Ejector pins push the solidified casting out of the mold.
If the ejector system does not work correctly, the casting may remain inside the mold or become deformed during ejection.
Common Problems
- Ejector pin sticking
- Uneven ejection
- Bent ejector pins
- Excessive ejector force
- Incorrect ejector pin position
Solutions
Keep the ejector system clean and properly lubricated.
Also, make sure the ejector pins are correctly aligned.
If the casting deforms during ejection, review the ejector pin layout and mold temperature before simply increasing ejector force.
Poor Mold Surface Quality
The mold cavity surface directly affects the final surface of the casting.
A damaged or contaminated cavity may cause:
- Rough surfaces
- Sticking
- Scratches
- Local marks
- Poor appearance
Therefore, regular cleaning and inspection are essential.
The cavity should be cleaned according to the mold material and surface treatment requirements.
Die Casting Mold Maintenance Checklist
Preventive maintenance can significantly reduce mold problems.
A practical maintenance checklist includes:
| Inspection Item | What to Check |
|---|---|
| Parting surface | Wear, damage, and flash |
| Cavity | Scratches, erosion, and contamination |
| Core | Wear and alignment |
| Gate | Erosion and blockage |
| Vent | Blockage and damage |
| Cooling channels | Flow and temperature |
| Ejector pins | Alignment and movement |
| Guide system | Wear and lubrication |
| Release agent | Spray coverage |
| Mold temperature | Stability during production |
By checking these items regularly, manufacturers can identify small problems before they become major mold failures.
How to Reduce Die Casting Mold Problems
The best way to reduce mold problems is to control the entire production process rather than fixing defects one by one.
1. Optimize Mold Design
Analyze metal flow, cooling, venting, and ejection before manufacturing the mold.
2. Control Mold Temperature
Keep the mold within a stable temperature range suitable for the alloy and casting design.
3. Maintain the Mold Regularly
Clean vents, inspect parting surfaces, check cores, and replace worn components.
4. Monitor the Die Casting Machine
Stable injection speed, pressure, and clamping force help maintain consistent production.
5. Control the Alloy
Use the correct alloy composition and control melting and holding conditions.
6. Record Mold Performance
Keep records of cycle count, repairs, defects, and replaced components.
This information can help predict maintenance needs and improve mold life.
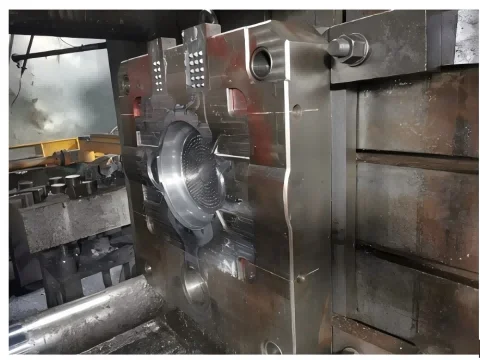
Die Casting Mold Problems: Quick Reference
| Problem | Main Cause | Solution |
|---|---|---|
| Porosity | Poor venting | Improve vents or vacuum |
| Flash | Mold gap or wear | Repair parting surface |
| Sticking | Poor release or high temperature | Adjust spraying and temperature |
| Erosion | High metal velocity | Optimize gate and flow |
| Heat checking | Thermal stress | Improve temperature control |
| Warpage | Uneven cooling | Balance cooling system |
| Cold shut | Low temperature or poor flow | Optimize temperature and gating |
| Dimensional deviation | Wear or misalignment | Inspect and repair mold |
| Ejector failure | Pin wear or misalignment | Repair ejector system |
| Rough surface | Cavity damage or contamination | Clean and polish cavity |
Conclusion
Die casting mold problems can affect casting quality, production efficiency, mold life, and manufacturing costs.
However, most problems can be controlled through good mold design, stable process parameters, proper temperature control, and preventive maintenance.
In practice, manufacturers should not treat a casting defect as an isolated problem. Instead, they should check the mold design, metal flow, temperature, injection parameters, venting, cooling, and ejection system together.
For high-volume production, this systematic approach can reduce scrap, extend mold life, and improve production stability.
If you are selecting a die casting machine and mold for a new project, Haichen can provide die casting machines, molds, and related auxiliary equipment based on your alloy, part size, production volume, and process requirements.


